Due to the cooling hopper being on the top end of the cylinder there is not the normal cylinder head arrangement on this engine. Instead the valves, plug and carburettor fit into a block on the side of the cylinder and there is a slot from that into the combustion chamber.
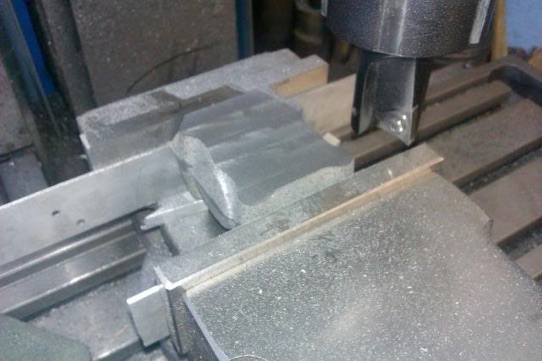
First job was to shim up the casting and get the surface that mates to the cylinder nice and flat. Due to the previously encountered chilled spots I used a carbide tipped ‘little hogger’ to do this.
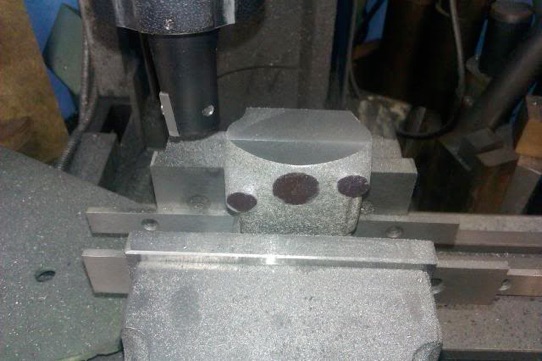
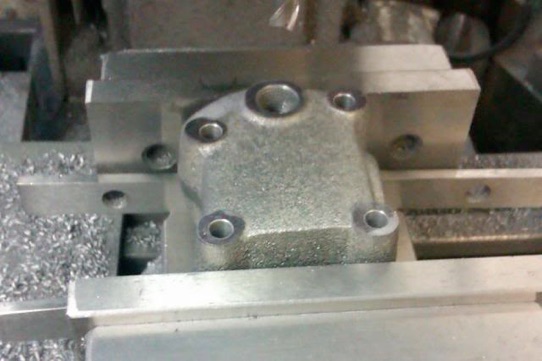
This flat surface was then placed against the vice fixed jaw, and the top machined flat.
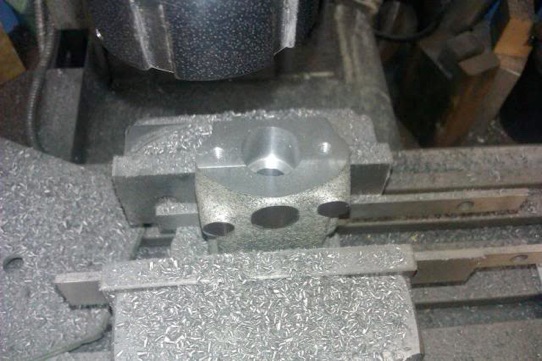
Followed by drilling and tapping the carb mounting holes and the larger hole which will create a space below the inlet valve where the fuel/air mixture is ignited (plug goes into the dark central boss on the front). The bottom of this hole has the seat for the exhaust valve and a hole right through for its stem.
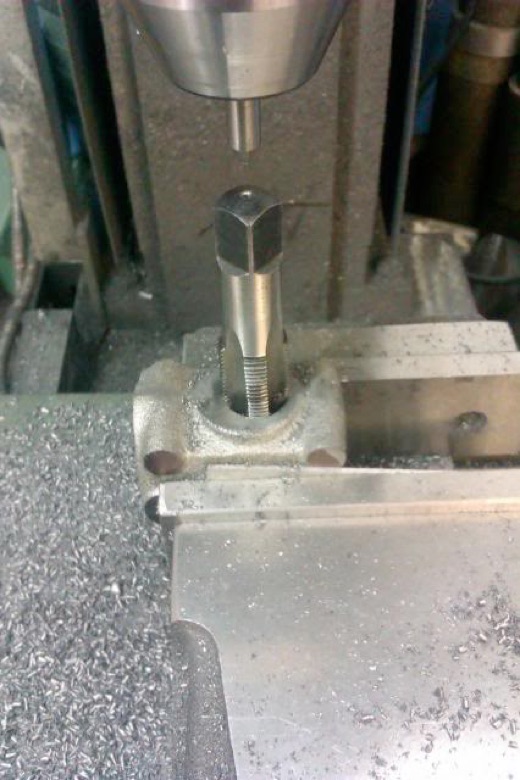
The casting was then turned 90degrees keeping the same face against the vice and the hole for the exhaust pipe drilled & tapped 3/8" BSP, using a pointed rod in the drill chuck to guide the tap. I find tapping like this better than a separate tapping guide/tool as you can always ensure the work is directly below the axis.
The last thing to do on this was to spot face the four mounting holes and spark plug hole, drill 3/16" for the 2BA studs and tap M10x1mm for the CM-6 plug.
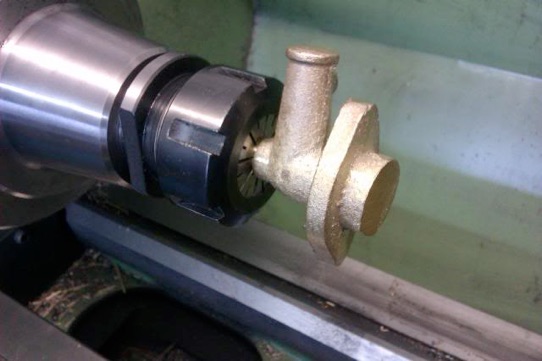
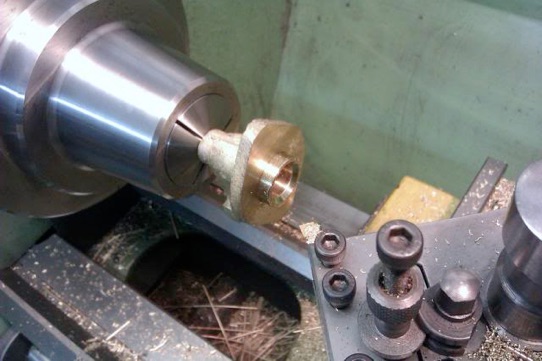
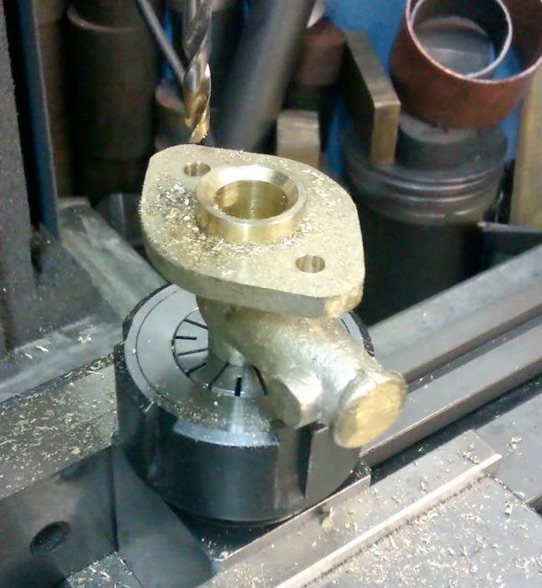
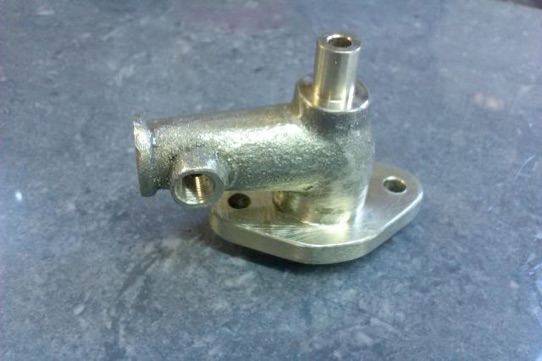
The carb also houses the inlet valve. A chucking spigot is provided and was lightly cleaned up with a file so it could be held in a collet, the end lightly faced and centre drilled so that the tailstock could give support while the boss and flange were turned.
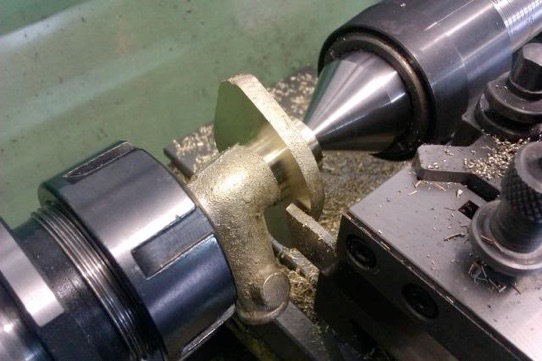
I also cleaned up the top face of the flange at the same time which needed to be done with a parting tool to clear the elbow.
I then held it by the spigot to machine the outside of the valve guide.
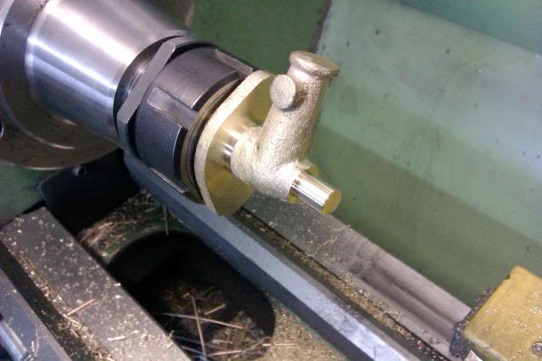
Flipping it back around again and held more firmly on the newly turned guide, the spigot and flange were given a final skim before drilling and reaming the hole for the valve stem, counter-boring and machining the valve seating.
Then over to the mill in a collet block to firstly drill the mounting holes...
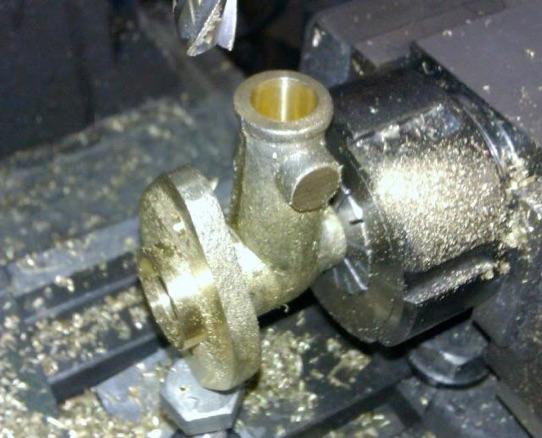
...and bore the intake at right angles to this.
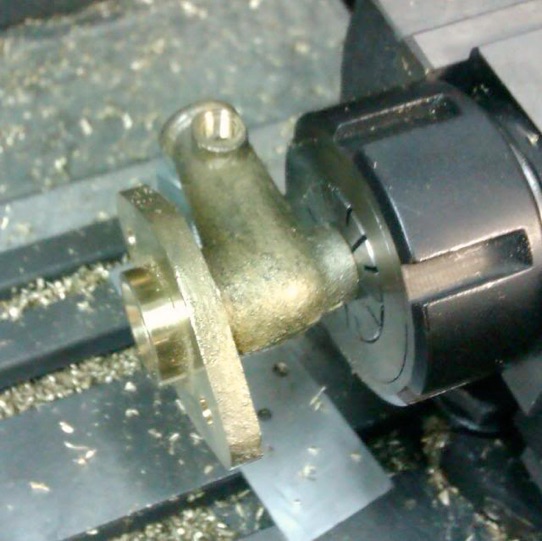
And then drill and tap for the needle valve body at right angles to the other two holes.
Part 1 part 2 part 3 Part 4 Part 5 Part 6 Part 7 Part 8 Part 9 Part 10 Part 11