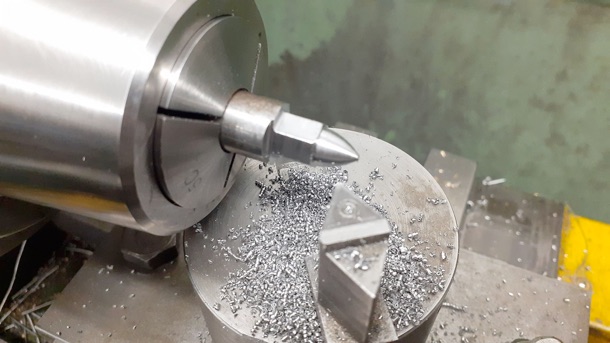
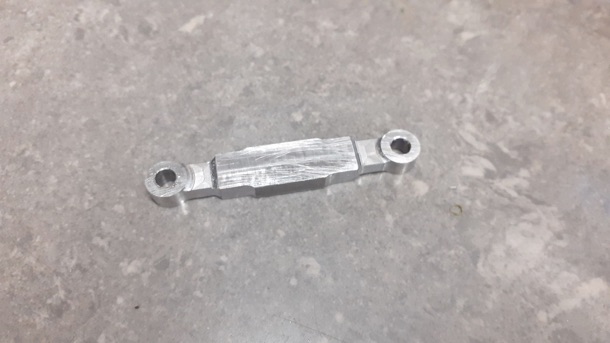
One small job that was next to be crossed off the list was making the acorn nuts for the tops of the columns. I started with some free cutting round bar and milled to a hexagon using the 5C indexer. The shaped top was cut with the ball turner before parting off and then holding the other way up to drill and tap the nut.
Next the valve gear starting with the levers that take the angled motion of the eccentric rod via a shaft to vertical movement that the valve requires. I actually made these links earlier as they served to show a couple of different options for CNC machining.
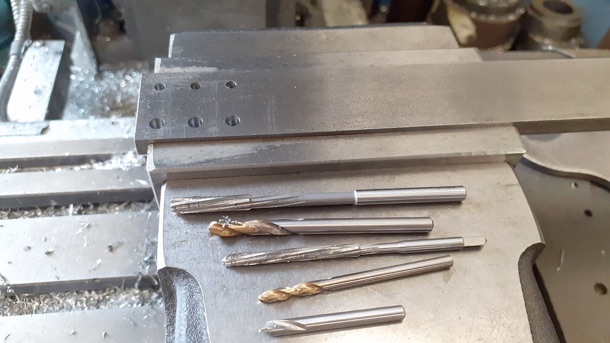
Starting with some 1/4" flat bar the holes for the three levers were spot drilled, then drilled with stub drills 0.2mm undersize and finally reamed.
The levers were then milled down to the required thickness, one at 5mm the other two at 6mm thick
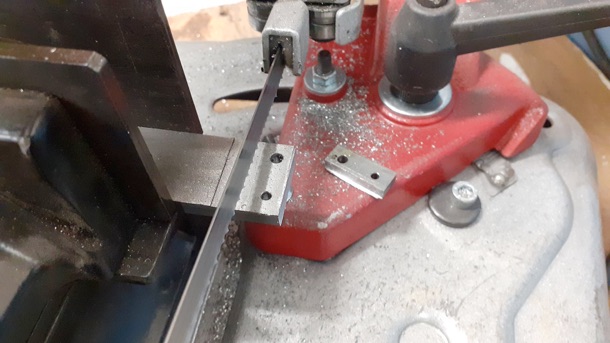
I then used the witness marks from milling to line up the band saw to cut the individual parts from the bar.
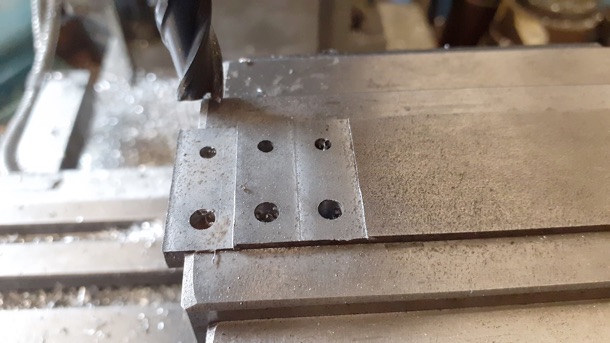
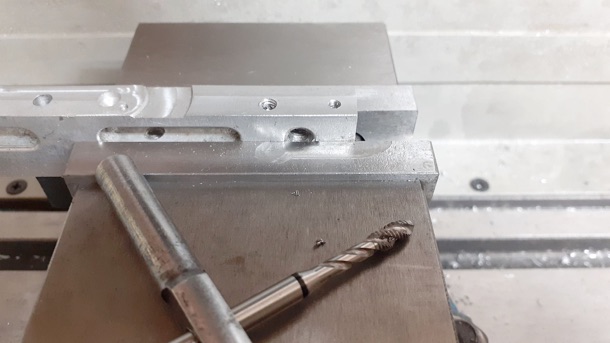
Over to the CNC and two holes were drilled and then manually tapped in a tooling block, this lines up the holes and sets one as datum which is easier than drilling manually and then having to locate the hole when the block is transferred to the mill.
I then ran two of the levers using an adaptive path to remove most of the material and then two contours of 0.2mm and then 0.1mm depth to finish the part this took 72seconds and as full depth cuts were used throughout the wear was spread along a reasonable length of flute. The last one I did as though the part were being cut from a larger sheet slowly ramping down to depth and then a contour to finish, this took 230seconds and almost all cutting was just with the end of the tool so wearing that short length more.
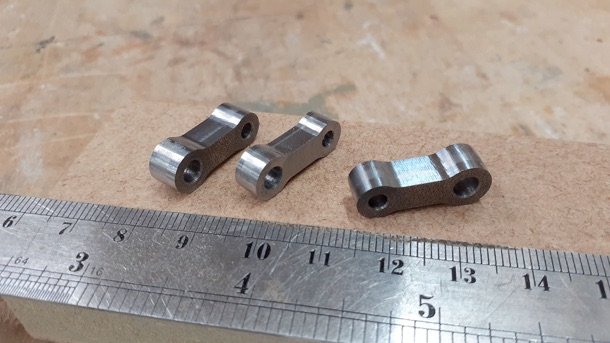
Stuarts show the levers with just straight edges but I went with a dog bone shape to add a bit more character as also stop them looking so bulky.
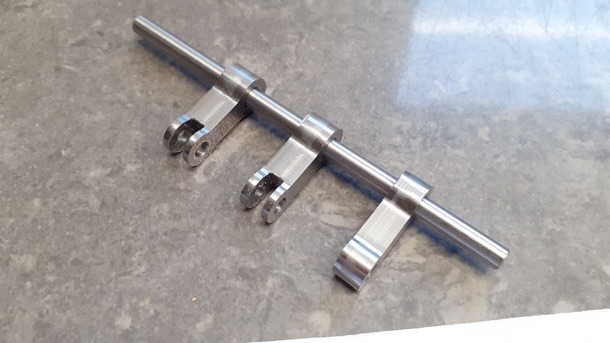
The final op was to mill slots for the vertical rods in the thicker two levers, and a thinner slot (still to be done) in the 5mm thick one for the eccentric rod.
Like the levers I gave the two blocks that support the cross shaft a bit more shape and as they looked a bit chunky also reduced the thickness between the round boss and the base. These were done from a bit of rectangular bar making use of the CNC again to get good transitions between the various radii. After this photo they were sawn off the bar, the base milled flat, and then drilled and tapped M2.5 for fixing studs.
.Part one here Part two Part three Part four Part five Part six Part seven